How Do You Qualify a Large Plastic Injection Mold Manufacturer?
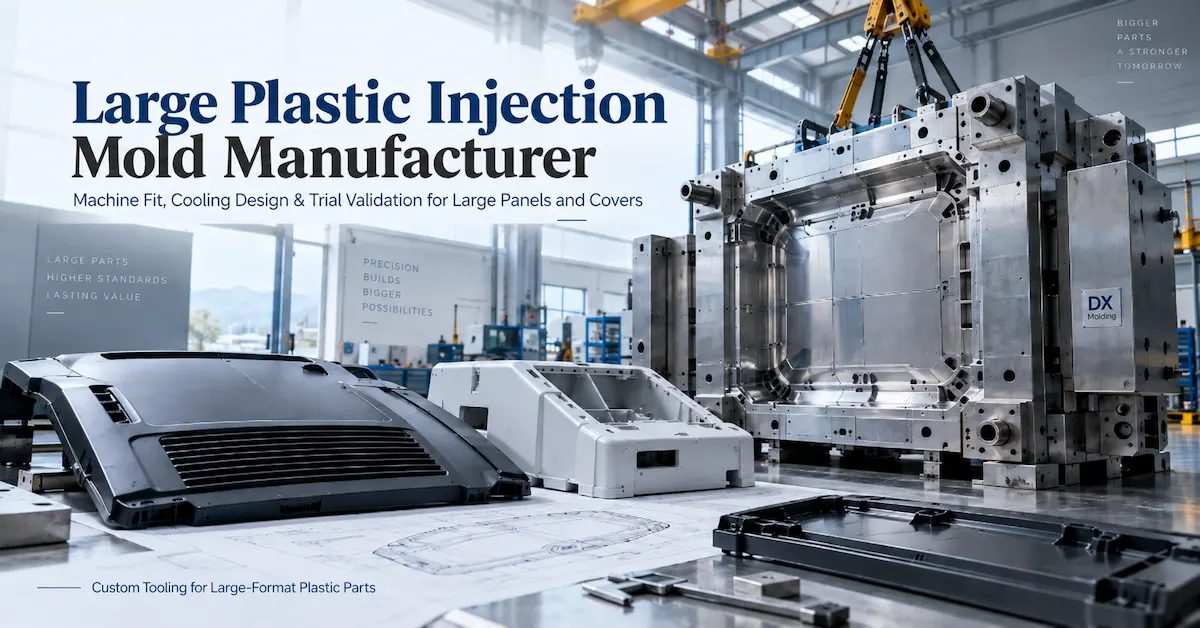
Qualify a large plastic injection mold manufacturer against the complete job: manufacturing the tool, assembling and handling it, running suitable trials, and measuring acceptable parts. The ability to machine a large cavity is not, by itself, evidence that every later step is covered. For panels and covers, establish the proposed mold dimensions, weight, machine requirements and acceptance method before relying on a delivery promise. DX Molding, operated by Shenzhen DongXin Technology Co., Ltd., provides custom plastic mold manufacturing, molded components and OEM/ODM development. Large-format inquiries still require project-specific confirmation of machining capacity, tool handling and trial arrangements; a general custom-molding service description is not a size or tonnage guarantee.
Which Projects Need a Large-Part Tooling Review?
This guide is intended for appliance OEMs, equipment manufacturers and contract molders evaluating wide panels, deep covers or substantial housing components. Consider three illustrative briefs—not claims about completed DX Molding projects. An appliance panel needs an agreed appearance and fit against its surrounding assembly. A deep equipment cover needs a defined opening and removal arrangement. An industrial housing needs mounting locations checked against its internal frame. Each brief should identify working conditions, cleaning exposure and any application tests. Separate tool-only procurement from a program that also includes molded-part supply. When the product architecture is still changing or the requirement is only a one-off prototype, review the development route before purchasing a production mold. Ask the large plastic injection mold manufacturer to identify unresolved design decisions rather than quote them as settled requirements.
Build a Large Injection Mold RFQ Around Measurable Inputs
An RFQ—a request for quotation—should make competing suppliers evaluate the same product and production arrangement. Use the following project specification checklist, not as a catalog specification or a statement of DX Molding’s capacity limits. Some fields come from the buyer; others require the supplier’s proposed design.
| Requirement | Buyer Input or Supplier Confirmation | What to Record |
|---|---|---|
| Part geometry | Current 3D model and controlled 2D drawing | Overall dimensions, depth and revision |
| Material | Exact resin grade or candidates requiring review | Fillers, color and permitted substitutions |
| Part and shot requirements | Part weight and proposed cavity/runner arrangement | Supplier’s total-shot assessment |
| Tool envelope | Proposed mold dimensions and weight | Confirmation against manufacturing and handling limits |
| Production equipment | Intended machine model and auxiliary equipment | Reviewed compatibility sheet |
| Functional geometry | Mating frame, mounting points and critical surfaces | Tolerances, datums and inspection method |
| Appearance | Visible surfaces, finish reference and acceptable marks | Cosmetic approval criteria |
| Demand | Launch quantity, reorder batches and annual forecast | Cavity and production assumptions |
| Tool construction | Steel, gates, cooling, inserts and moving components | Approved mold specification |
| Validation and delivery | Trial scope, fixtures, reports and tool destination | Acceptance and handover requirements |
Do not invent missing dimensions, material grades or cycle times to complete the form. Mark them for review, identify who supplies the answer, and retain the same revision across quotations. A large plastic injection mold manufacturer should distinguish a preliminary estimate from an offer based on an approved specification.
Check Manufacturing Capacity and Machine Fit Separately
Verify the Toolmaking Route
Request the proposed route through machining, electrical discharge machining where needed, fitting, assembly and inspection. For each substantial component, ask whether the equipment can accommodate its dimensions and weight together with the required workholding. Establish which operations are performed internally and which require an outside facility. Ask how externally processed components return to the controlled inspection process. DX Molding’s mold factory audit guide explains why equipment photographs alone do not demonstrate manufacturing control. For this project, request confirmation of the relevant working envelopes and inspection arrangements—not just the longest CNC axis on the machine list.
Review More Than Clamping Tonnage
Have the toolmaker and intended molder review clamp requirements, total shot, platen and tie-bar clearances, mold thickness, opening stroke and ejection interfaces. A deep cover also needs an agreed removal path once the mold opens. Include cooling connections, controller requirements and handling equipment in the review. These are separate checks: sufficient clamping force does not establish adequate opening travel or confirm every interface. DX Molding’s export mold compatibility guidance identifies these machine and handover considerations. Ask your large plastic injection mold manufacturer to name the proposed trial machine and document differences from the intended production setup.
Resolve Filling, Cooling and Release Risks Before Steel Cutting
Review Long Flow Paths and Gate Locations
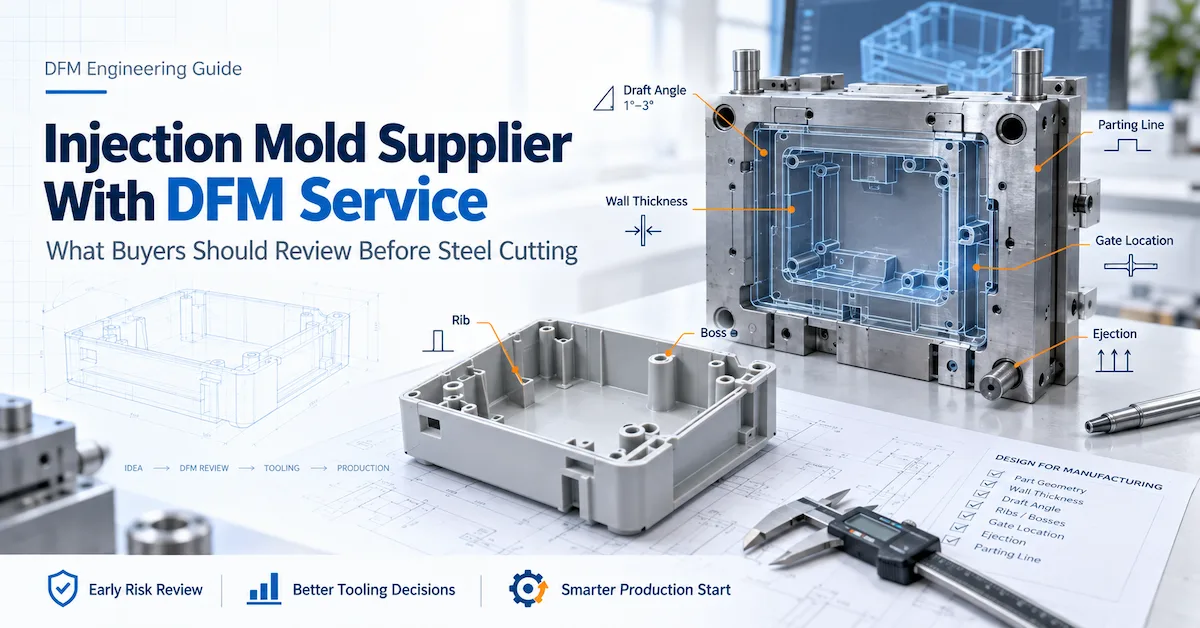
Start the design-for-manufacturing review, or DFM, with the resin grade, wall sections, proposed gates and cosmetic restrictions. Ask where filling finishes, where flow fronts meet, and which changes are recommended before machining. Large components may justify multiple injection points or sequential valve gating, but neither should be specified merely because the part is large. The proposed system needs a reason tied to filling behavior, appearance and production conditions. DX Molding’s hot runner mold guide discusses these choices, including the additional control and maintenance requirements of valve gates. Require the analysis to identify its assumptions and the decisions it changes.
Connect Cooling to Panel Shape
Large flat surfaces deserve particular attention to cooling distribution. Local thickness around ribs, bosses or corners can create different cooling and shrinkage behavior from the surrounding wall. Review those features together rather than attempting to solve an exterior distortion without examining the structure behind it. DX Molding’s plastic enclosure molding guide explains the relationship between cooling, wall geometry and dimensional stability. Ask for the proposed cooling layout, access for maintenance and the trial measurements that will test the plan. A cooling diagram is a design proposal; accepted molded samples provide the later evidence.
Include Venting and Part Release
Have the design review identify end-of-fill regions, deep features and the intended venting approach. Review draft, texture, ejection locations and moving components before approving visible surfaces. DX Molding’s engineering support covers manufacturability review, mold-flow analysis, ejection planning and cooling layout. Confirm the analysis and deliverables included in your specific project rather than assuming every service applies automatically.
Specify Resin and Tool Steel as Different Decisions
For large plastic injection molding, record the production resin separately from the mold materials. DX Molding lists ABS, PP, PC, nylon and other plastics for custom molded parts, while its plastic injection mold options include P20, H13 and S136 steels. These lists are starting points for project review, not interchangeable approvals. Ask the large plastic injection mold manufacturer to identify the proposed core, cavity, insert and wear-component materials and explain their selection. Agree on material documentation, heat-treatment requirements where applicable, surface finishing and replacement components. Distinguish a mold-life design target from an agreed commercial guarantee, including maintenance and wear-part assumptions. A familiar steel name does not answer all those questions.
Compare Tooling Concepts, Not Just Bigger Specifications
The following comparison concerns custom tooling configurations rather than standard product models. The options are not mutually exclusive: cavity count, feed system and insert construction are separate design choices that can be combined. Use the table to question the proposal rather than select a configuration without reviewing the part. DX Molding’s guides discuss two-plate tooling, hot runners and multi-cavity production as different engineering decisions.
| Configuration | Potential Benefit | Main Trade-Off | Question Before Approval |
|---|---|---|---|
| Single-cavity cold-runner tool | Relatively straightforward feed system where suitable | Runner handling and material usage | Does the gating arrangement meet fill and appearance requirements? |
| Single-cavity hot-runner tool | Can reduce cold-runner material in suitable programs | Additional controls, components and maintenance | Does the production case justify the added equipment? |
| Multiple valve-gate arrangement | Greater control over individual gate timing | More complex setup and servicing | What filling or cosmetic requirement does the sequence address? |
| Multi-cavity tool | Multiple identical parts per cycle | Machine capacity and cavity consistency | Can the complete mold and shot run on the intended machine? |
| Replaceable-insert construction | Localized servicing or agreed feature changes | Insert interfaces and additional fitting requirements | Which changes or wear areas are actually covered? |
A large plastic injection mold manufacturer should explain how the recommended combination meets your forecast, equipment and acceptance criteria. Review actual output needs before increasing cavity count, and identify the spare parts and documentation required for the selected system.
Approve Large Parts in the Correct Measurement Condition
Consider a hypothetical equipment cover that becomes flat only when four screws pull it against a frame. That may demonstrate an assembled-fit condition, but it does not establish free-state flatness. Specify which condition matters, where the part is supported, and when it is measured after molding. Ask the large plastic injection mold manufacturer to propose an inspection method covering the complete part and its critical interfaces. DX Molding’s dimensional-control guide distinguishes mold accuracy from finished-part performance and emphasizes dimensional and assembly validation.
Agree a production-representative trial and sampling plan rather than approving one selected component. Link results to the drawing revision, resin, machine and processing record, and identify unresolved appearance, dimensional or operating issues. DX Molding publishes trial-reporting, dimensional-inspection and process-record support; confirm the deliverables and measurement range for your project. Where certificates or test reports are required, request the actual documents and check their scope. Neither a general quality statement nor a certificate logo establishes large-mold capability.
Plan Capacity, Delivery and Handling Before Tool Completion
Ask your large plastic injection mold manufacturer for dates covering design release, material procurement, machining, fitting, first trial, corrections, approval and dispatch. For each resource-dependent stage, ask which facility or machine is planned and whether its availability is confirmed. DX Molding’s project workflow separates requirements review, DFM, manufacturing, trials and production; use those stages to structure the schedule rather than treating first samples and final approval as the same milestone.
For a substantial mold, add a documented handling and transport review. Ask the responsible specialists to confirm the finished tool weight, lifting and installation arrangements, packing dimensions, protection method and receiving-site access. Include the mold drawing, cooling diagram, component list and agreed spares in the handover register. Resolve who supplies each item before the mold is ready to leave the workshop.
Compare Large Injection Mold Cost Through Accepted Production
Compare the same engineering, tooling and delivery scope before ranking quotations. Separate design work, steel, purchased systems, trials, corrections, inspection, fixtures, spares and packing. For a program including molded parts, add production assumptions and packaging requirements. Ask a large plastic injection mold manufacturer how its cycle estimate will be demonstrated, and whether the estimate includes the complete molding and removal sequence. Consider this hypothetical planning calculation, not a DX Molding performance claim: for 150,000 shots, a 15-second cycle difference represents 150,000 × 15 ÷ 3,600 = 625 machine hours. The example excludes setup, downtime and rejected parts. It shows why an unverified cycle assumption deserves scrutiny alongside the tooling price; it does not prove that a faster cycle is achievable. Accept a cycle target only together with the required part quality, resin and trial conditions.
Define OEM, ODM and Engineering-Change Responsibilities
For an OEM program, identify the released product drawing and require approval before functional geometry changes. For an ODM program, also assign responsibility for mechanical design, prototypes and the decision to proceed into tooling. DX Molding’s services include product development, structure review and prototyping alongside mold manufacture. Before appointing a large plastic injection mold manufacturer, distinguish a correction needed to meet an approved requirement from a buyer-requested revision after approval. Record cost, schedule and revalidation consequences before authorizing changes. Also define mold ownership, document delivery, maintenance, storage and transfer arrangements. For large tooling, request a written assessment of whether a proposed change affects the entire tool, a replaceable component or the intended machine setup.
Send DX Molding a Drawing-Based Feasibility Brief
To discuss a large-format project, send your current 3D model, 2D drawing, overall part dimensions, resin requirement, expected quantity and intended production location. Include mating-part information, visible surfaces and the main issue you need reviewed—such as panel distortion, a deep draw, a restricted gate location or uncertainty about machine fit. State whether you need an export mold or finished-part production. DX Molding accepts drawings, samples and project requirements for feasibility discussions. Request a large plastic mold project review and ask for project-specific confirmation of tool size, manufacturing route and trial arrangements before proceeding.
Frequently Asked Questions
1. What Should a Large Plastic Injection Mold Manufacturer Confirm Before Quoting?
Provide the part’s dimensions and depth, the proposed tool dimensions and weight, material, cavity plan and receiving-machine information. Use those measurable requirements rather than assuming that the word “large” communicates the same scope to every supplier.
2. What Is the Maximum Mold Size DX Molding Can Manufacture?
The general service descriptions linked here do not establish a verified maximum tool dimension, weight or press tonnage. Request written confirmation against your drawings, including machining, assembly, handling, inspection and trial requirements, before treating the project as accepted.
3. Is Machine Tonnage Enough to Confirm Compatibility?
No. Review the complete machine specification, including mold dimensions, opening travel, ejection and total-shot requirements. Have the toolmaker and receiving molder approve the specific arrangement rather than relying on the clamping-force number alone.
4. Does Every Large Plastic Part Need a Hot Runner?
No. Evaluate the resin, geometry, gating requirements, production quantity and maintenance implications. Multiple valve gates may help selected projects, but the size label alone does not justify that configuration. Require an engineering explanation and trial validation.
5. How Should We Address Warpage in a Large Panel?
Review wall geometry, ribs, local thickness and cooling together, then validate the proposed solution on molded samples. Define the measurement and assembly conditions first so the supplier is solving the actual acceptance problem.
6. Can Large Molded Parts Have Tight Tolerances?
Define tolerances around functional requirements and assess them for the actual material, geometry and process. Do not apply a mold-machining capability figure to every finished-part dimension. Agree on the inspection method and validate the critical features during trials.
7. How Much Does a Large Injection Mold Cost?
Request a quotation after the tool concept, resin, volume and quality requirements have been reviewed. Compare included engineering, purchased systems, trials, corrections and handover items. Without that matched scope, two headline prices may describe different projects.
8. How Long Does a Large Mold Take to Complete?
Request a project schedule rather than a universal duration. Distinguish design approval, first trial, corrective work, approved samples and shipment, and identify the resources and buyer decisions controlling each milestone. Changes should trigger an updated schedule.
9. Can DX Molding Supply the Tool and Molded Parts?
DX Molding lists both custom mold manufacturing and plastic-part production. For a large component, confirm the particular mold and production requirements before selecting that arrangement; the general service offering does not establish capacity for every proposed size.
10. Can an Existing Large Mold Be Modified?
Submit its available drawings, condition information, samples and proposed change for review. Ask for confirmation of machining access, affected components, handling requirements and revalidation. DX Molding lists modification-feasibility evaluation among its support services; acceptance remains project-specific.
Conclusion
Choosing a large plastic injection mold manufacturer means verifying the complete route from the proposed tool to an accepted molded part. For wide panels and deep covers, prioritize manufacturing and machine compatibility, filling and cooling decisions, measurement conditions and trial evidence. Compare cost and timing only after those assumptions are clear, and do not substitute a general factory claim for confirmation of the actual tool size and production arrangement. Send DX Molding your CAD files, material, quantities and intended molding-machine details to begin a project-specific review of the tooling requirements and open engineering questions.