
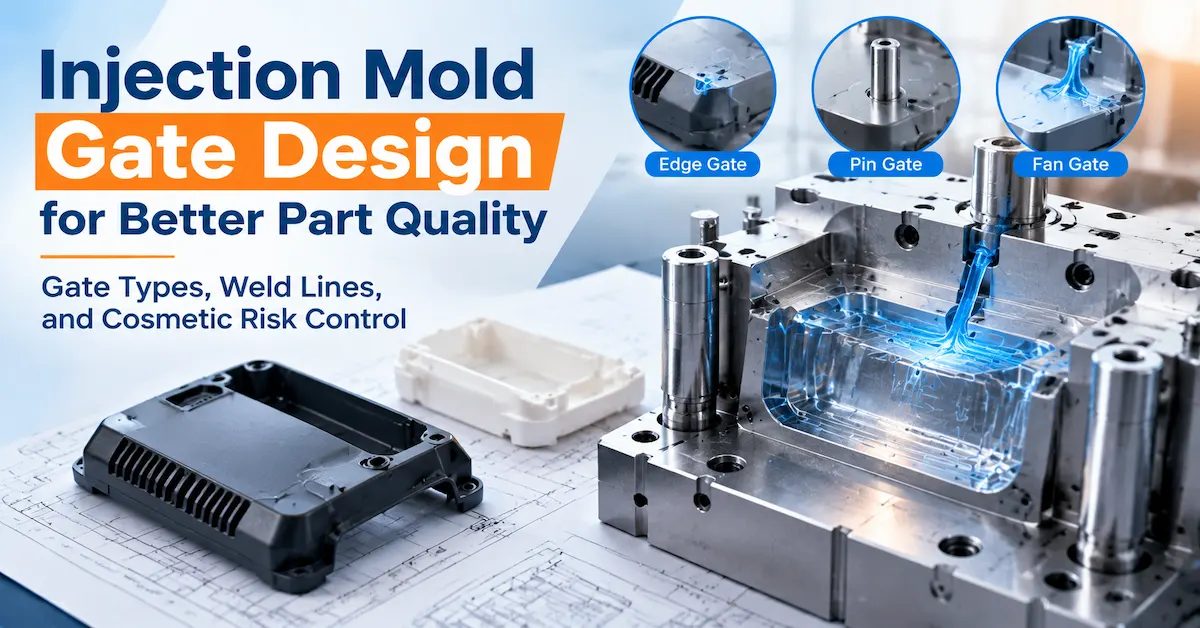
What Does Injection Mold Gate Design Control?
Injection mold gate design controls the transition from the runner system into the cavity. At that transition, the plastic flow begins to spread through the part geometry. The gate therefore connects the mold's feeding system to the molded part's quality requirements. A design that fills a simple, hidden bracket may be unsuitable for a large textured cover, a clear lens, a thin wall, a glass-filled structural part, or a multi-cavity cosmetic component.
The gate affects several linked stages:
- Filling: the gate influences where the melt enters, how the flow front travels, and where multiple fronts meet.
- Packing: the gate controls how pressure reaches the cavity and how long the material can be packed before the gate freezes.
- Cooling: the local gate and runner geometry can create a thicker or hotter region that needs to be considered with the cooling layout.
- Appearance: a gate may leave a witness mark, blush, jetting line, blush-like blemish, read-through, or trimming trace.
- Dimensions: filling and packing differences can affect shrinkage, flatness, hole position, fit, and part-to-part variation.
- Fiber and filler orientation: flow direction can influence anisotropic shrinkage and mechanical behavior in reinforced materials.
- Automation: the gate and runner concept must work with degating, trimming, part removal, inspection, and packaging.
These effects are linked. Moving a gate can hide a mark but lengthen the flow path; adding a gate can reduce flow length but create a weld line; changing to a hot runner can open new gate options while adding thermal controls and maintenance. A useful review makes those trade-offs visible before the mold is frozen.
Gate location is a product decision
Buyers sometimes treat gate location as an internal tooling decision that can be left to the supplier. That approach is risky when the part has an A-surface, a sealing edge, a connector opening, a transparent region, a snap fit, a bearing surface, or a customer-facing logo. Gate vestige can be acceptable on an internal rib and unacceptable on an exterior panel. The same gate mark can be harmless on a hidden appliance bracket and a rejection point on a visible consumer enclosure.
Before the supplier finalizes the concept, mark the following on the controlled product model:
- Visible surfaces and surfaces hidden after assembly.
- Sealing, sliding, bearing, optical, and electrical contact surfaces.
- Critical dimensions and inspection datums.
- Allowed gate, ejector, parting-line, and overflow marks.
- Areas where a weld line is functionally or cosmetically unacceptable.
- Material direction or fiber-orientation concerns.
- Assembly interfaces and mating parts.
This information gives the mold designer a quality map instead of a neutral CAD file. Without it, the supplier may optimize for filling alone while the buyer later evaluates a visible gate mark, weld line, or distortion that was never defined at the design stage.

How to Select a Gate Before Tooling Release
There is no universal best gate. Gate selection should be based on a documented relationship between the product, material, production plan, and acceptance criteria. The following table provides a practical starting point for a tooling review. It describes common engineering tendencies, not universal performance guarantees.
| Gate type | Typical fit | Quality questions to resolve | Buyer risk if selected without review |
|---|---|---|---|
| Edge gate | Parts with a suitable edge or parting-line feed area | Gate mark, flow length, packing, trimming, and weld-line location | Visible vestige or an unbalanced fill path |
| Fan gate | Wide flat regions where a broad flow front is useful | Gate spread, shear, trimming, and cosmetic uniformity | A large gate area that is difficult to hide or trim consistently |
| Tab gate | Parts needing a controlled transition into the cavity | Tab removal, stress, gate blush, and the effect on appearance | A secondary tab operation or inconsistent break-off |
| Submarine or tunnel gate | Automatic degating from a side, rib, or hidden area | Tunnel angle, steel strength, gate vestige, and mold maintenance | Gate breakage, difficult machining, or an unacceptable mark |
| Pin-point gate | Three-plate or suitable hot-runner arrangements with small gate points | Gate blush, vestige, stress, gate freeze, and automatic separation | A small mark in a visible area or process sensitivity around the gate |
| Direct or sprue gate | Large or thick sections where a direct feed is acceptable | Gate vestige, packing concentration, stress, and removal method | A prominent mark or localized shrinkage on a cosmetic surface |
| Hot-tip gate | Hot-runner layouts where a controlled point feed is appropriate | Thermal balance, stringing, drool, gate freeze, and service access | Thermal instability or an exposed hot-tip mark |
| Valve gate | High-control or multi-gate programs where timing and vestige matter | Valve timing, weld lines, gate sequencing, maintenance, and cost | More components and controls than the program actually needs |
| Film or ring gate | Certain broad, annular, or rotationally symmetric geometries | Uniformity, trimming, knit-line avoidance, and circular distortion | Complex trimming or a broad gate witness around the part |
Edge gates
An edge gate feeds from the side, often through the parting plane. It can suit rectangular components, plates, covers, and parts with a hidden perimeter. Review the flow length, far-side weld lines, gate visibility, trimming method, and any functional opening in the flow path. Show the gate on the product model and define the allowable vestige on the drawing or cosmetic standard.
Fan gates and tab gates
A fan gate spreads the entrance over a wider area and can suit broad flat regions. A tab gate creates an intermediate feature that can control the transition and be removed after molding. Both require an agreed trimming method: a fan gate may leave a wide witness, while a tab gate may need a secondary operation or controlled break-off. A gate that fills well but cracks the edge during degating is not a successful design.
Submarine or tunnel gates
A submarine or tunnel gate enters through an angled passage and can support automatic degating from a side wall, rib, or hidden area. Review tunnel angle, steel strength, gate access, ejection, break-off consistency, and vestige. Ask whether the tunnel is in a replaceable insert and how the gate will be inspected and maintained.
Pin-point gates
A pin-point gate is a small point feed often used with three-plate or suitable hot-runner structures. It can support automatic separation, but its small size may increase sensitivity to material temperature, fill speed, pressure, gate freeze, and local surface condition. It is not automatically invisible; define the acceptable blush, stress mark, raised point, or flow pattern with a visual standard.
Direct and sprue gates
A direct or sprue gate feeds a larger section from the sprue or a direct hot-runner connection. It can suit thick, large, or structurally simple parts where a prominent gate is hidden or acceptable. For a cosmetic panel, review localized packing, gate vestige, sink, stress, dimensional effect, and the removal method.
Hot-tip and valve gates
Hot-tip gates add heated manifold and nozzle options; valve gates add mechanical opening and closing control for programs where timing, weld-line placement, vestige, or cavity filling needs more control. Neither is an automatic quality upgrade. Review temperature control, valve timing, gate condition, leakage risk, service access, spares, and maintenance against the actual production strategy.
How Gate Design Creates or Reduces Weld Lines
A weld line forms when two or more flow fronts meet and do not fully fuse as one continuous front. Depending on material, temperature, pressure, surface condition, fiber content, geometry, and process settings, the meeting line can be mainly cosmetic, a dimensional concern, or a functional weakness. It may appear near a hole, boss, insert, rib, side action, or other obstacle that divides the flow.
Gate design influences weld lines in three ways:
- It determines the starting point of flow. Changing the gate location changes the path the material takes around holes, ribs, and thick-to-thin transitions.
- It determines whether one or multiple fronts meet. A single gate can still create a weld line when the flow divides around an obstruction. Multiple gates make the meeting location a deliberate design issue.
- It affects the condition at the meeting point. The angle, temperature, pressure, venting, and timing of the fronts influence whether the line is acceptable.
For a housing with a connector opening, an edge gate may send fronts around the opening and create a weld line behind it. Moving the gate could hide that line but lengthen the flow path, change the gate mark, or alter packing near the connector. Compare the whole part-quality map before choosing.
Weld-line risk review
Ask the tooling supplier to identify predicted weld-line locations on the product CAD or a filling-analysis image when analysis is part of the agreed scope. The review should distinguish between a predicted meeting line and an actual unacceptable defect. A risk record should state:
- Where the weld line is expected.
- Which feature creates the split flow.
- Whether the location is cosmetic, structural, sealing, or dimensional.
- What gate, runner, vent, overflow, or process change is proposed.
- Whether the buyer must approve a product change.
- How the result will be checked at T0, T1, T2, or the agreed trial stages.
Moving the gate is not the only solution. Venting, a local radius or wall change, process settings, or an overflow tab may improve the meeting area when the product and trimming plan allow it. Evaluate every option against tooling cost, appearance, function, maintenance, and change control.
Weld lines in glass-filled or reinforced materials
Reinforced materials add a material-direction question. Fibers may orient with the flow, and a weld area may have a different local orientation from the surrounding part. The buyer should identify load-bearing features and avoid assuming that a visually small line is mechanically irrelevant. The actual effect depends on resin grade, filler content, geometry, process conditions, and the design's load case.
For reinforced structural parts, include the resin grade and the critical load direction in the RFQ. Ask whether the gate location supports the required orientation and whether the weld-line area should be kept away from a boss, hinge, snap arm, fastener, or load path. If a material supplier's data sheet or customer standard defines specific testing, include it in the acceptance plan instead of relying on a visual judgment alone.
How Gate Design Affects Cosmetic Appearance
Gate-related appearance problems are often discovered late because the first mold review focuses on fill and tool construction. A part can be dimensionally close to nominal and still fail because the gate mark, blush, weld line, gloss difference, flow mark, or trimming trace is visible from the customer's normal viewing direction.
Gate vestige and gate mark
Every gate concept should answer three questions: where is the remaining mark, how is it removed, and what is the acceptance limit? A concealed gate can still affect assembly if the remnant interferes with a mating part. A side gate can be acceptable on a hidden wall but not on the edge that users touch. A hot-tip gate can be small but visible. A valve gate can reduce certain marks but still needs a defined gate appearance.
Do not use the phrase “no gate mark” unless the buyer has defined the actual requirement. Injection molding normally leaves some evidence of the feed point or its removal. The correct requirement may be “gate mark allowed on non-cosmetic internal surface,” “no sharp projection,” “flush after trimming,” or “visual mark not visible at the specified inspection distance.” These are different requirements and lead to different designs.
Flow marks, jetting, and gloss variation
The local flow entering the cavity can affect surface appearance. A narrow or poorly oriented entrance may create a visible flow trace or jetting-like pattern, particularly when the material shoots into an open area before contacting the cavity wall. The gate design, gate direction, local wall geometry, fill speed, melt condition, mold temperature, and texture all interact.
For textured parts, the texture direction and draft must be reviewed with the gate and flow direction. A gate change after texture is finalized may change the visible flow pattern or highlight a region that had previously been hidden. A buyer should approve the visual reference part and texture specification together with the gate location rather than approving them as unrelated documents.
Sink and read-through near the gate
A gate can be close to a thick boss, rib, pad, or local mass. Packing pressure may improve one region while the thick feature cools and shrinks differently from the surrounding wall. The visible symptom can be sink, read-through, gloss change, or a local depression. The gate is not always the only cause, but its position can affect how pressure reaches the region.
Review the gate together with wall thickness, rib-to-wall ratio, boss design, core-out options, cooling distance, and ejection. If a gate must be close to a thick feature, record the expected risk and define how the cosmetic surface will be inspected. If the buyer cannot accept a mark or sink there, the product geometry or gate location may need to change before steel cutting.
Gate Design and Part Quality: A Practical Comparison
The table below helps buyers compare gate concepts using quality questions rather than only tooling terminology. The “best fit” column is intentionally conditional. A supplier should confirm the decision against the actual CAD, resin, volume, cavity plan, and machine.
| Buyer requirement | Gate discussion | Evidence to request |
|---|---|---|
| Visible Class A or textured surface | Place the gate outside the normal viewing area and review flow traces and weld lines | Marked CAD view, cosmetic standard, and approved sample criteria |
| Long thin housing | Compare flow length, pressure loss, gate count, venting, and likely weld lines | Filling review, gate layout, and risk register |
| Sealing or snap-fit interface | Keep vestige and weld lines away from functional interfaces where practical | Critical-feature map and assembly inspection plan |
| Glass-filled structural part | Review flow direction, weld-line location, fiber orientation, and load path | Material grade, load case, gate rationale, and agreed validation method |
| High-volume production | Compare cavity balance, automatic degating, cycle assumptions, maintenance, and waste | Runner concept, cavity balance plan, maintenance access, and trial records |
| Very low visible vestige | Compare pin-point, hot tip, valve, submarine, or hidden edge options | Gate-mark reference, trimming method, and sample approval criteria |
Two Illustrative Gate Design Cases
The following cases show how a buyer can reason through a gate decision. They are engineering examples created for this guide. They do not represent a named DX Molding customer, a guaranteed result, or a published factory performance claim.
Case 1: Electronics housing with a visible top cover
A product team submits a two-piece electronics housing. The top cover is visible after assembly, the lower shell contains bosses, and a connector opening sits near one end. A proposed side gate on the top cover would leave a witness on a visible edge and could send flow toward the connector opening.
The review should separate the requirements: the top exterior is cosmetic, the connector opening controls assembly, and the hidden lower shell can accept a gate mark. The supplier can compare a hidden edge gate, a tunnel gate into an internal rib, and a hot-tip or fan-gate option if volume and runner strategy justify it. The approval record should show the gate, flow direction, weld-line risk, venting, degating, and cosmetic inspection points.
Case 2: Multi-cavity bracket with a load-bearing boss
A second illustrative part is a multi-cavity bracket with a load-bearing boss and side opening. A small pin-point gate would separate automatically, but the proposed position would send two fronts to the boss root. The decision must therefore include cavity balance, weld-line position, boss strength, packing, and dimensional consistency.
Request a cavity-by-cavity plan showing the gate and runner layout, expected weld line, critical boss dimension, inspection method, sample quantity, and the rule for correcting a cavity mismatch. One acceptable sample from one cavity does not prove the complete tool is ready.
Gate Design Review Checklist Before Steel Cutting
Use this checklist in a DFM or mold-design review. A “yes” answer is not enough by itself; the evidence and approval owner should also be recorded.
| No. | Review question | Required evidence | Approval owner |
|---|---|---|---|
| 1 | Is the gate type identified? | Gate and runner layout with type, location, and intended degating method | Tooling engineer |
| 2 | Is the gate mark acceptable? | Product view showing cosmetic, hidden, functional, and touch surfaces | Product and quality teams |
| 3 | Where will weld lines occur? | Flow review, analysis result where included, or an explicitly stated engineering prediction | Tooling and product engineering |
| 4 | Are weld lines away from critical features? | Overlay of weld-line locations against holes, bosses, seals, snaps, and load paths | Product engineer |
| 5 | Is venting sufficient near the last-fill and meeting areas? | Vent locations, air-trap risk, and flash or maintenance considerations | Tooling engineer |
| 6 | Does the gate support packing of critical dimensions? | Gate-freeze assumption, critical dimensions, and process validation plan | Process and quality teams |
| 7 | Is the gate compatible with the resin? | Resin grade, filler content, processing window, and material handling requirements | Materials and process teams |
| 8 | Is the runner and cavity layout balanced? | Cavity layout, runner lengths, gate sequence, and balance assumptions | Tooling and production teams |
| 9 | Can the part be degated and inspected consistently? | Degating method, operator or automation steps, and visual standard | Production and quality teams |
| 10 | Does the tooling document show the approved gate? | Approved 3D mold assembly, 2D drawing, BOM, and revision record | Buyer and tooling supplier |
| 11 | Is the trial acceptance plan defined? | T0/T1/T2 checks, appearance limits, critical dimensions, and sample traceability | Buyer quality team |
| 12 | Are open risks assigned and dated? | Risk register with action, owner, due date, and closure evidence | Project manager |
What Evidence Should a Tooling Supplier Provide?
A credible gate-design review should produce traceable evidence rather than a verbal recommendation. The package will vary by project, but buyers can request:
- A product CAD view with the proposed gate locations and gate types.
- A runner and cavity layout showing how the feed system connects to the cavities.
- A written gate rationale covering resin, geometry, appearance, production quantity, and automation.
- A weld-line and air-trap risk review, with analysis results when analysis is included in the quotation.
- A cosmetic risk map showing gate marks, weld lines, ejector marks, parting lines, and texture areas.
- A list of assumptions, including material grade, shrinkage input, part revision, and acceptance criteria.
- A DFM revision record showing which issues are approved, open, rejected, or moved to trial validation.
- Trial documentation that connects the gate design to appearance inspection, critical dimensions, and modification follow-up.
DX Molding's published project-support information describes DFM and tooling review, mold assemblies, 2D engineering drawings, spare-parts BOM information, T0/T1/T2 trial reporting, dimensional inspection, appearance-defect records, CMM data where applicable, modification follow-up, and process-parameter records. These are published support capabilities, not a promise that every item is included in every quotation. Confirm the exact deliverables and inspection method before the purchase order.
DX Molding identifies itself as Shenzhen DongXin Technology Co., Ltd., founded in 2007, with support for custom plastic injection molds, molded plastic components, silicone tooling, and OEM/ODM development. The relevant point for gate design is the engineering handoff: gate decisions should connect the product model to mold design, trials, inspection, and production. Its website identifies Shenzhen, China, as its location and provides project contact routes.
Prepare a better gate-design RFQ. Include the material grade, annual volume, cavity target, visible surfaces, gate-mark limits, critical features, mating parts, and required trial documents.
Send CAD and Quality RequirementsHow Gate Design Is Validated During Mold Trials
Gate approval is an engineering decision, not proof that the first molded parts satisfy every requirement. Trial molding provides physical evidence. Connect each sample to the tool revision, material, process condition, cavity, and inspection method because gate marks, weld lines, and dimensions can change with those variables.
At T0: verify the mold mechanism and basic fill
The first trial should confirm opening, closing, movement, venting, ejection, and basic filling. Record short shots, flash, air traps, incomplete gate opening, runner problems, jetting, and obvious weld lines as a baseline rather than a final product-quality judgment.
At T1: check appearance and critical geometry
At the next stage, compare the part with the drawing, cosmetic standard, and assembly references. Check gate vestige after actual degating, inspect weld lines against the risk map, and measure critical features with the defined method. CMM data can support dimensional review where applicable, but does not alone prove cosmetic or functional acceptance.
At T2 or final validation: confirm closure and repeatability
Later trials should verify completed modifications against the acceptance plan. A useful closure record states what changed, why, which tool revision, material, process, and cavity were used, and how the result was judged.
For multi-cavity tools, identify samples by cavity. Runner balance, gate condition, cooling, or processing variation can produce different vestige, weld-line, or dimensional results between cavities.
How to Include Gate Requirements in an RFQ
A vague RFQ forces the supplier to fill in missing decisions. A useful RFQ gives enough information to propose a gate concept and lets the buyer compare quotations on equal terms.
Product and material inputs
- Controlled 3D CAD and 2D drawing revision.
- Resin manufacturer, grade, color, filler, and recycled-content requirement if applicable.
- Annual volume, order quantity, expected tool life, and future variants.
- Machine information or the intended production machine range.
- Parting-line limitations, side-action restrictions, and automation requirements.
Quality and appearance inputs
- A-surface and B-surface definitions.
- Allowed gate and trim locations.
- Areas where weld lines, flow marks, sink, or blush are unacceptable.
- Critical dimensions, datums, assembly interfaces, and inspection method.
- Surface texture, gloss, color, and visual inspection conditions.
- Functional load paths, seals, snaps, hinges, bosses, and electrical interfaces.
Tooling and validation inputs
- Preferred or open evaluation of cold runner, hot runner, valve gate, or other feed systems.
- Required DFM, 3D mold design, 2D drawings, BOM, and spare-parts documentation.
- Required gate-design review milestone before steel cutting.
- T0/T1/T2 or equivalent trial stages and sample quantities.
- Appearance, dimensional, assembly, and functional acceptance criteria.
- Tool ownership, transfer requirements, maintenance access, and change control.
Ask each supplier to separate confirmed facts, engineering assumptions, proposed options, and open buyer decisions. This distinction prevents a preliminary gate concept from being mistaken for an approved manufacturing requirement.
Frequently Asked Questions About Injection Mold Gate Design
Which injection mold gate type is best for cosmetic plastic parts?
There is no universal best type. A hidden edge, tunnel, fan, pin-point, hot-tip, or valve gate may fit depending on geometry, resin, volume, runner system, and the allowed mark. Choose against the visible-surface, weld-line, dimensional, degating, and maintenance requirements, and show the proposed gate on the product model.
How can gate design reduce weld lines?
Gate design can reduce weld-line risk by changing the flow starting point, redirecting split flow, changing gate count or sequence, and keeping meeting fronts away from critical features. Venting, geometry, process settings, and material conditions also matter. A new location may create a longer flow path, a different mark, or a packing problem.
Can a gate be placed on a visible surface?
It can be, if the product requirement allows the mark and removal is controlled. Define the visual inspection condition and limit. For a Class A or customer-facing surface, compare hidden options or document why a visible gate is necessary; a small mark can still fail in the normal viewing direction.
Is a hot runner always better than a cold runner?
No. A hot runner may reduce cold-runner waste or support a higher-volume gate arrangement, but it adds thermal components, controls, service requirements, and maintenance. A cold runner may fit a simpler or lower-volume project. Compare material, cavity count, appearance, cycle strategy, maintenance, and total tooling scope.
How do I specify gate quality in a mold quotation?
Specify gate type and location, acceptable mark, allowed surfaces, weld-line limits, trimming method, runner concept, cavity identification, trial checks, and approval evidence. Include a controlled drawing or marked CAD view. Undecided items should remain open rather than becoming supplier assumptions.
What should I send to a tooling supplier for a gate review?
Send the latest 3D CAD, controlled drawing, material grade, color and filler information, quantity, machine information, visible-surface map, critical dimensions, mating parts, texture, allowed gate locations, and required validation documents. Identify whether it is a new tool, transfer, modification, or production investigation.
Does CMM inspection prove that gate design is correct?
No. CMM data can verify defined dimensions when the method and datums are appropriate, but it does not prove that gate mark, weld line, appearance, material orientation, or assembly function is acceptable. Combine dimensional inspection with appearance, assembly, process, and functional checks.
Conclusion
Injection mold gate design affects more than where plastic enters the cavity. It influences the flow path, packing, cooling, weld-line position, gate vestige, cosmetic appearance, dimensional behavior, fiber orientation, degating method, cavity balance, and long-term tooling maintenance. A gate concept should therefore be approved as part of the product and tooling system, not as an isolated feature on a mold drawing.
For buyers, the most reliable process is to define visible and functional surfaces, provide the correct material and production inputs, compare gate options against the actual CAD, record predicted weld-line and air-trap risks, and connect the gate decision to T0/T1/T2 trial evidence. Ask the supplier to distinguish confirmed information from assumptions, show the gate on the product model, and close each important risk with an owner and an inspection method.
act before tooling?
Share your CAD revision, resin, volume, critical surfaces, and inspection requirements for a project-specific discussion.
Discuss Your Injection Mold Tooling Project



